A camera module can pass a sample evaluation and still fail a product launch if the supplier cannot repeat that result across thousands of units. That is why a factory inspection is not a ceremonial supplier visit. For OEMs, product managers, and engineering teams, it is a direct check of whether a manufacturer can control the details that determine image quality, yield, delivery performance, and long-term field reliability.
For compact imaging products, small process variations matter. A dust particle on a sensor, unstable lens focus, inconsistent adhesive dispensing, or incomplete electrical testing can produce costly failures after assembly. The goal is not simply to confirm that a factory looks organized. It is to verify that people, equipment, documentation, and quality gates work together at production scale.
What a Factory Inspection Should Prove
A useful inspection answers a practical question: can this supplier manufacture the exact camera module required, at the requested volume, with evidence of repeatable control? The answer should come from production records and observed processes, not broad assurances.
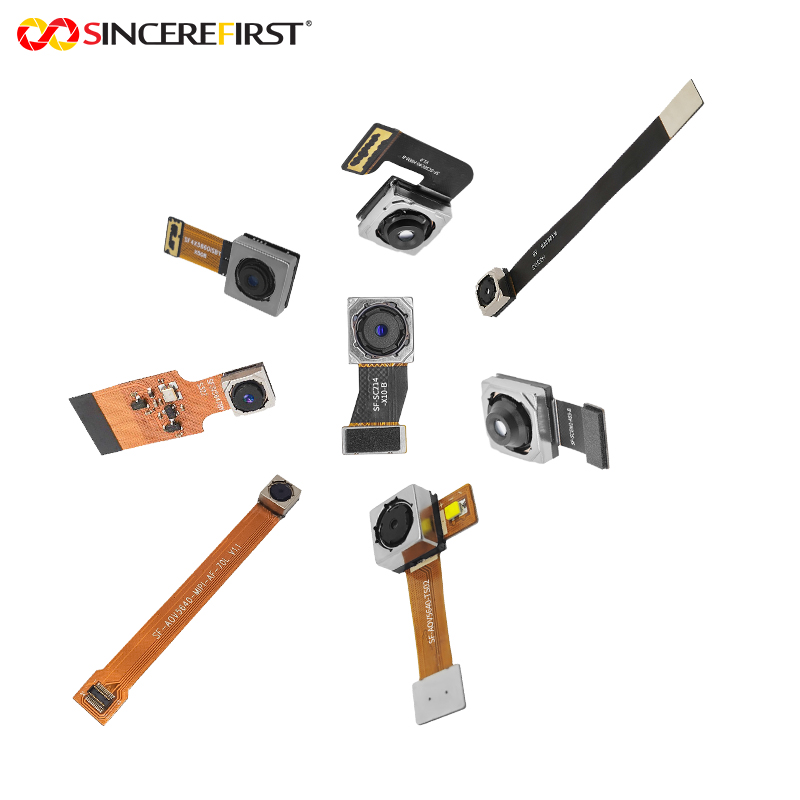
For camera modules, buyers should assess more than the final assembly area. A capable facility manages incoming materials, cleanroom discipline, optical alignment, active focus where required, image testing, aging, packaging, and shipment traceability. If the supplier offers customized MIPI, USB, DVP, FPC, medical, or endoscope modules, the inspection should also show how engineering changes move from prototype approval into controlled mass production.
A supplier may have an impressive sample room but limited production discipline. Conversely, a high-volume factory may be highly efficient with standard modules while being poorly equipped to support low-volume customization. Neither condition is automatically disqualifying. The right fit depends on whether the program needs rapid iteration, a stable catalog part, specialized optical performance, or sustained high-volume output.
Factory Inspection Checklist for Camera Modules
Start with process flow, not the reception area
Ask to see the complete material and manufacturing flow, from incoming inspection through finished-goods release. This reveals whether the factory has built quality into the process or relies mainly on final inspection to catch defects.
Incoming controls should cover image sensors, lenses, PCBs, connectors, FPCs, adhesives, filters, and packaging materials. Inspect how lots are labeled, quarantined, sampled, and released. A camera module manufacturer should be able to trace a finished unit back to the key component lots used during assembly. That level of traceability becomes especially valuable when investigating a field issue or managing an engineering change.
Observe how sensitive components are stored and handled. Sensors and PCBs require electrostatic discharge protection. Adhesives may need controlled storage and defined use periods. Optical components need protection from fingerprints, scratches, and contamination. If personnel are improvising labels, storage locations, or handling methods, production consistency is at risk even when the final product appears acceptable.
Verify cleanroom and contamination control
Image defects are often manufacturing defects in disguise. Dust, fibers, oil residue, and uncontrolled airflow can create black spots, flare, uneven shading, or cosmetic failures that become visible only under certain scenes or lighting conditions.
The inspection should confirm the cleanliness standard appropriate for the module type and application. Look for gowning procedures, air filtration, cleaning schedules, material transfer rules, sticky mats, controlled work surfaces, and disciplined operator behavior. For endoscope and medical imaging modules, where optical paths are compact and quality expectations are high, contamination control deserves particularly close attention.
Cleanroom classification alone is not enough. Ask how the factory monitors the environment, how often it cleans critical stations, and what happens when contamination is detected. The practical evidence is more meaningful than a sign on the door.
Review optical assembly and focus capability
Lens-to-sensor alignment is central to camera module performance. The factory should explain whether focus is fixed, manually adjusted, mechanically locked, or set through active alignment. Each approach has trade-offs.
Fixed-focus modules can be efficient and cost-effective for defined working distances, but the lens specification, assembly tolerances, and focus verification method must match the application. Active alignment can support demanding optical performance, especially when depth of field, edge sharpness, or tight field-of-view tolerance matters, but it adds equipment, cycle-time, and process-control requirements.
During the visit, inspect the alignment equipment and the criteria used to accept or reject modules. Ask what image targets are used, how sharpness is measured across the field, how focus drift is prevented after curing, and how lens torque or adhesive volume is controlled. A supplier should be able to relate optical test results to the product specification rather than relying on subjective visual checks.
Examine electrical and image-quality testing
A complete test plan verifies both electronic function and visible image performance. For a USB or UVC camera module, that may include interface detection, frame rate, resolution, current consumption, and image output. For MIPI or DVP modules, testing should also address timing, signal integrity, driver compatibility, and target-platform behavior where applicable.
Image-quality testing should be matched to the use case. Common checks include dead or stuck pixels, white balance, color consistency, exposure response, signal-to-noise ratio, shading, distortion, resolution, and dark-current behavior. The exact test mix depends on the sensor, lens, illumination conditions, and application. A security camera and a medical imaging module should not be qualified against the same priorities.
Ask whether tests are performed on every unit, by sampling, or at defined production stages. One hundred percent functional testing may be justified for mission-critical or high-cost modules, while a statistically controlled plan can be more economical for mature, high-volume products. What matters is that the test coverage reflects the actual failure modes and customer requirements.
Check calibration, maintenance, and data integrity
Test equipment is only as trustworthy as its calibration and maintenance system. Review calibration labels, due dates, equipment records, and procedures for handling out-of-calibration instruments. This applies to optical test stations, electrical fixtures, torque tools, environmental chambers, and measurement devices.
Also ask how test data is retained. A mature operation can link test results, defect codes, rework records, and shipment details to a production lot or serial number. Data visibility allows the manufacturer to identify drift before it becomes a large-scale quality issue. It also makes root-cause analysis faster when a customer reports a failure.
Questions That Reveal Manufacturing Readiness
The most revealing questions are specific. Instead of asking whether a supplier has quality control, ask for the top three defect categories from recent production, the corrective actions taken, and the evidence that those actions worked. Instead of asking whether capacity is sufficient, ask about available lines, cycle time, staffing plans, equipment bottlenecks, and the lead time for scaling output.
Engineering change control is equally important. Camera modules frequently require adjustments to sensor selection, lens parameters, cable length, connector orientation, firmware settings, mechanical dimensions, or packaging. Confirm how a revised drawing, bill of materials, and test specification are approved before production resumes. Uncontrolled changes are a common source of version mismatches between an approved sample and delivered product.
For regulated or demanding applications, ask how nonconforming material is identified and segregated, who can approve rework, and whether rework data is tracked. Rework is not inherently unacceptable. The concern is unrecorded rework that changes performance or hides a recurring process problem.
Match the Inspection to Your Program Stage
An early supplier assessment should focus on technical capability, engineering communication, sample turnaround, and whether the factory understands the intended use environment. At this stage, buyers should confirm that a custom design can be manufactured, not just designed.
Before mass production, the inspection should become more process-specific. Review pilot-run yield, first-article records, work instructions, test fixtures, packaging validation, and approved control plans. If production is already running, focus on yield trends, capacity utilization, delivery performance, customer-return handling, and traceability depth.
Remote factory audits can be useful when travel is impractical, particularly for an initial qualification. Live video walkthroughs, document review, and real-time demonstrations can establish a baseline. They do not fully replace an on-site inspection for complex modules, high volumes, medical applications, or programs with tight optical tolerances. Physical observation often exposes details that a prepared video tour does not.
Turn Findings Into a Stronger Supply Agreement
A factory inspection has value only when findings lead to clear production expectations. Record the agreed revision level, acceptance criteria, test requirements, defect limits, traceability format, packaging specification, and change-notification process. For custom camera modules, include the approved golden sample and the conditions under which it was evaluated.
SincereFirst approaches this work as an engineering and manufacturing discipline: confirm the imaging requirement early, build the necessary controls into the process, and maintain visibility as output scales. Buyers benefit most when their supplier treats inspection feedback as input for measurable improvement, not as a one-time audit exercise.
The most productive factory visit ends with fewer assumptions. When process controls, optical testing, and accountability are visible on the production floor, your team can move from supplier uncertainty to a camera module program built for repeatable delivery.